RPZ Valve
Established in 2000, Hubei RPZ Valve Co., Ltd. is a leading manufacturer and exporter specializing in the design, development, and production of high-quality OEM & ODM metal products. With over 20 years of experience in production and international trade, we have established a solid reputation for delivering precision-engineered valve components and other metal products.
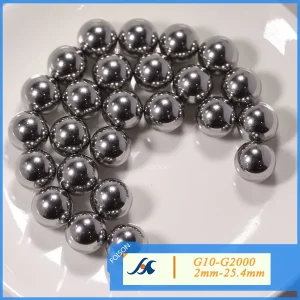
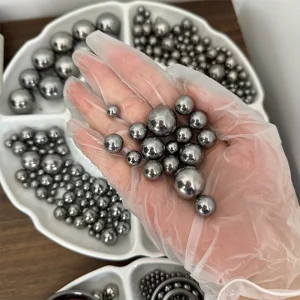
Our product range includes a variety of valves, valve balls, valve stems, disk springs, bonnets, and more. While valve balls are our core offering, we are also capable of producing a wide array of other metal products tailored to the specific needs of our clients. We pride ourselves on our flexibility and commitment to providing customized solutions based on customer requirements.
International buyers are increasingly demanding high-durability dewatering valve components capable of withstanding extreme pressure and corrosive environments in mining, municipal engineering, and heavy industrial wastewater systems.
Integration of advanced metallurgy, ceramic coatings (such as alumina ceramic solutions), and precision CNC manufacturing ensures zero-leakage performance, extending operational life cycles significantly.
Global engineering firms require custom dimensions, special alloy selections (304, 316, tungsten carbide, and specialized polymers), and rigorous testing protocols tailored to unique hydraulic layouts.
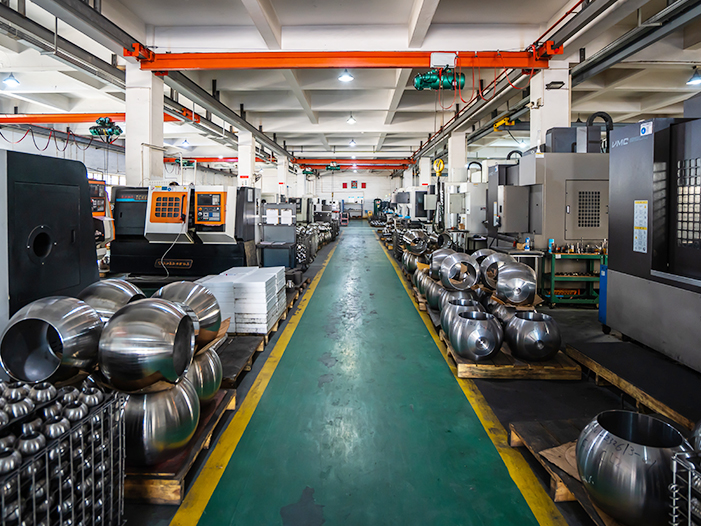
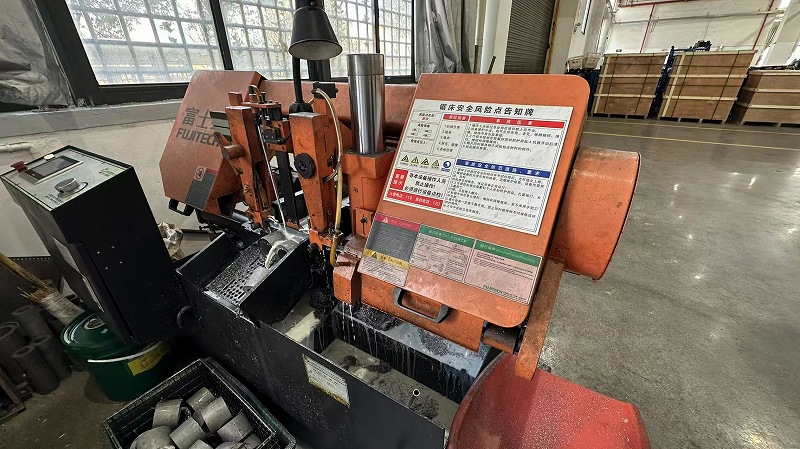
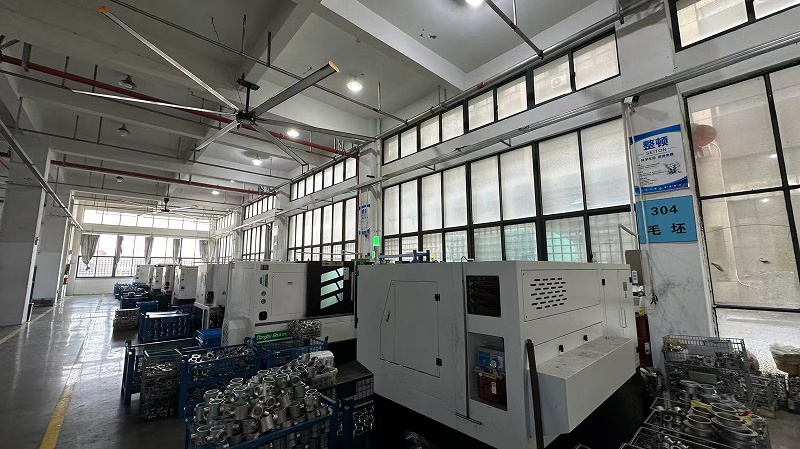
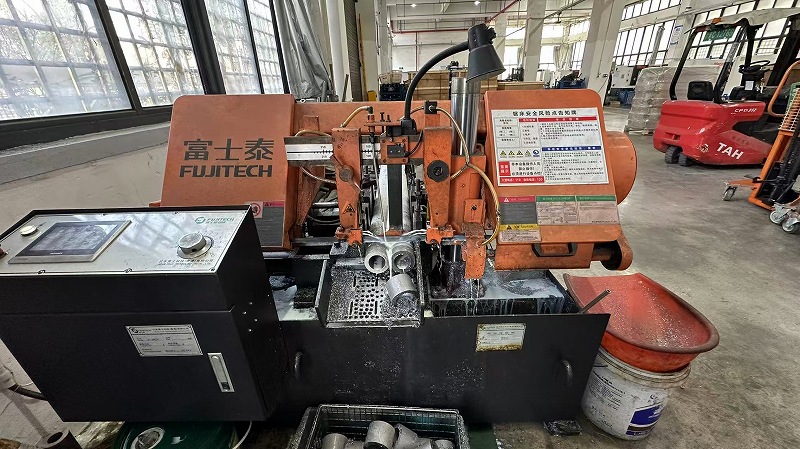
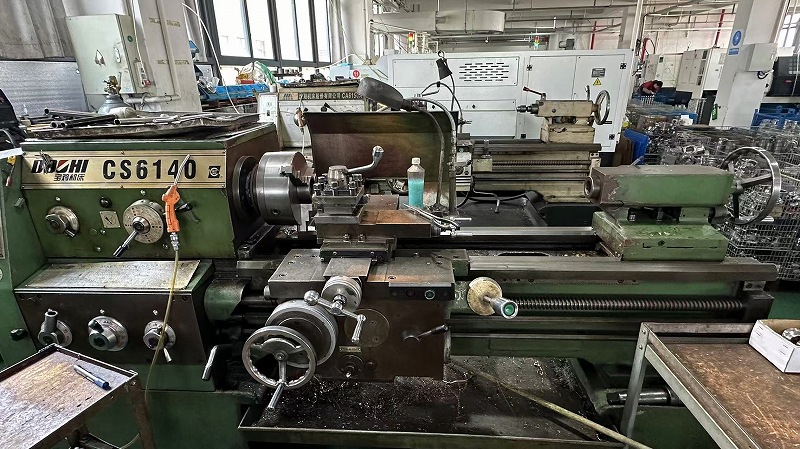
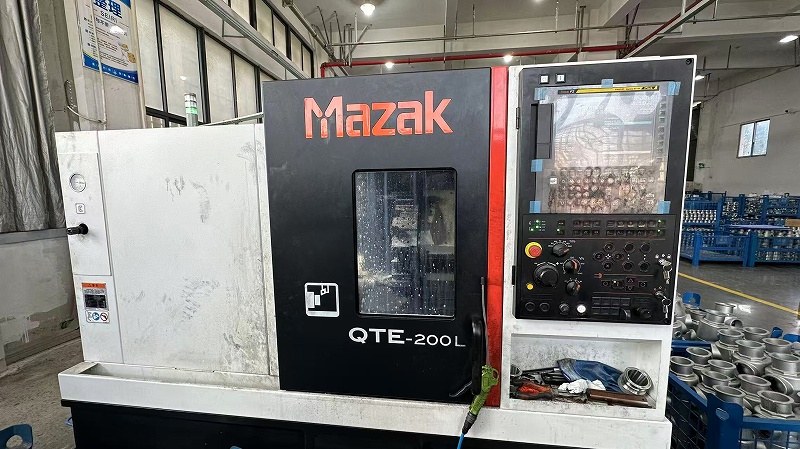
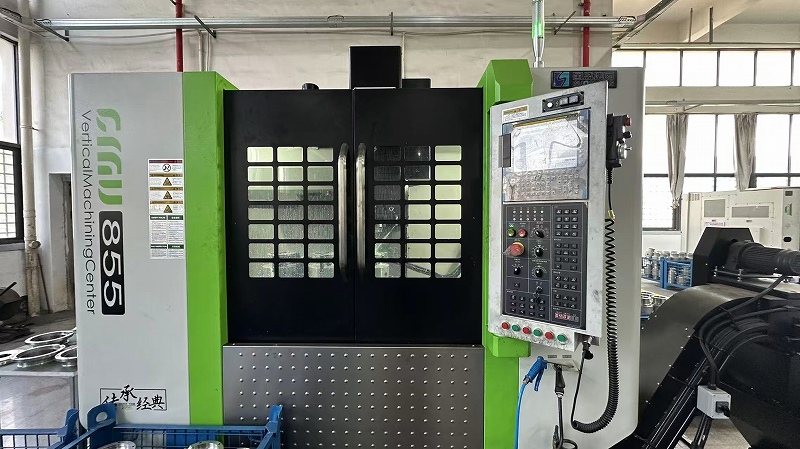
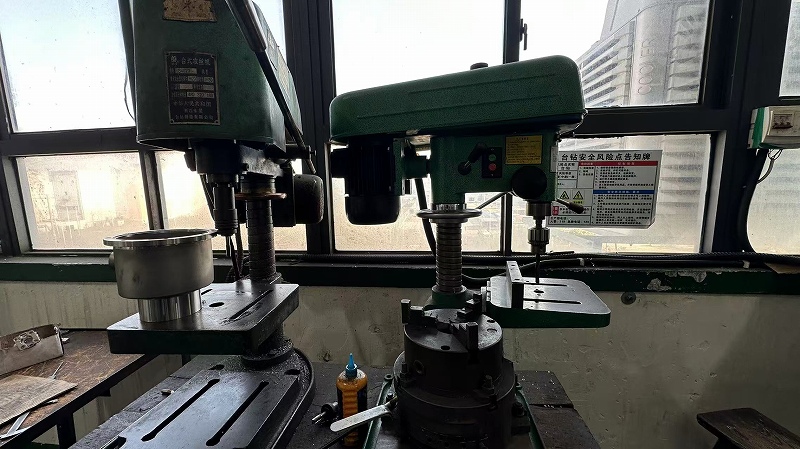
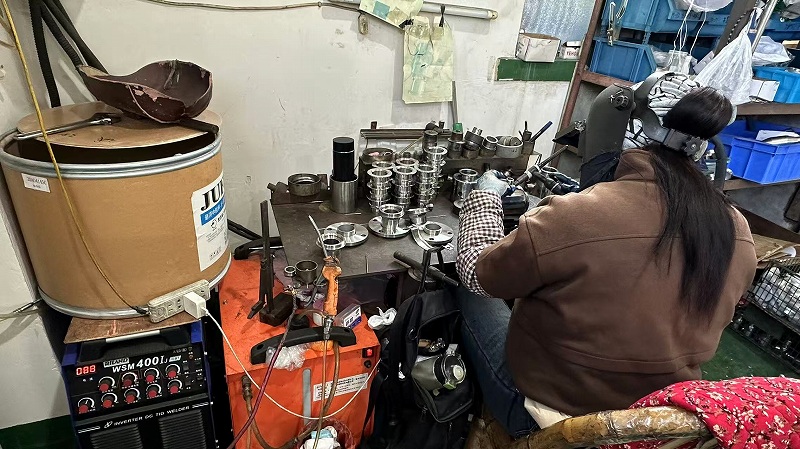
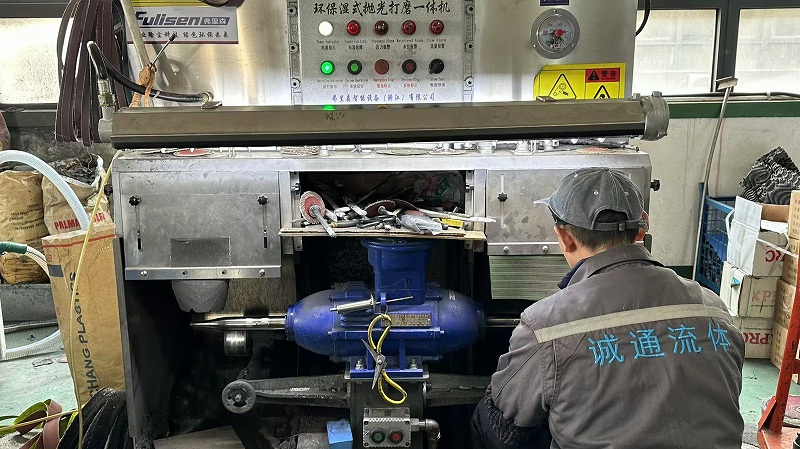
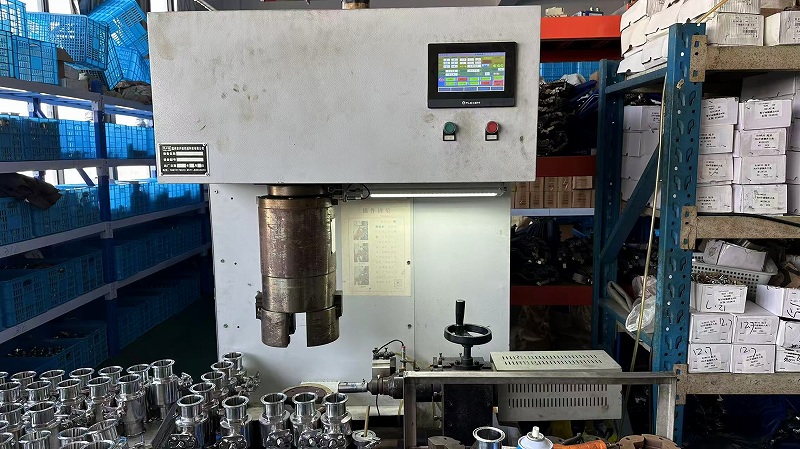
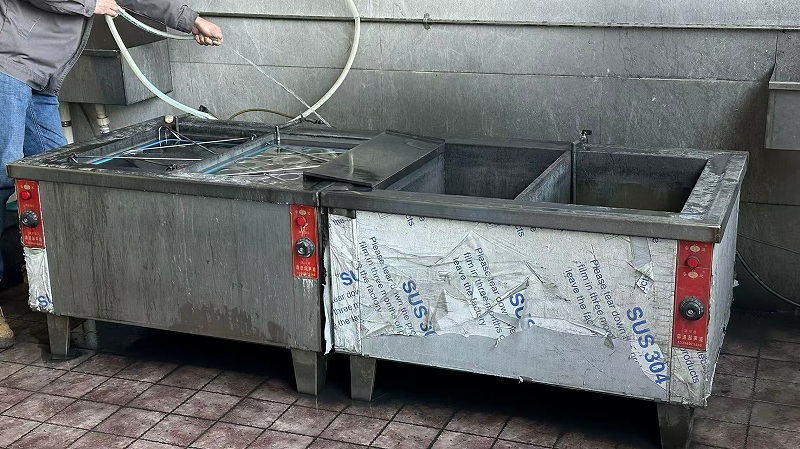
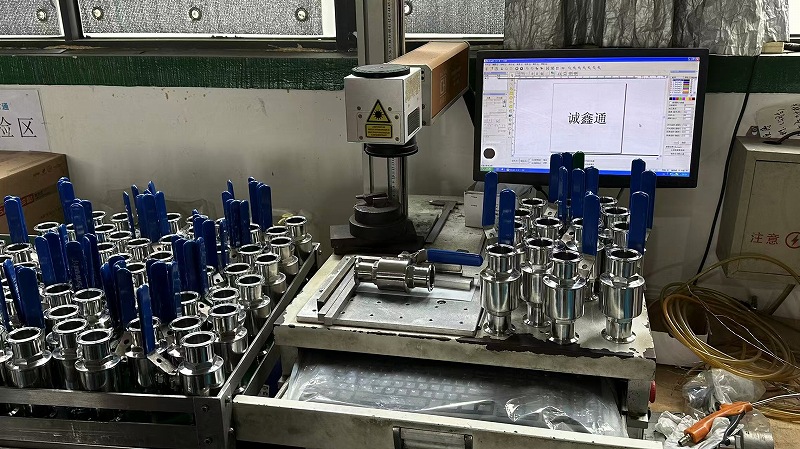
At Hubei RPZ Valve Co., Ltd., we operate our own affiliated factories equipped with cutting-edge machinery and technologies. Over the years, we have invested heavily in enhancing our manufacturing capabilities to meet evolving global demands with superior consistency.
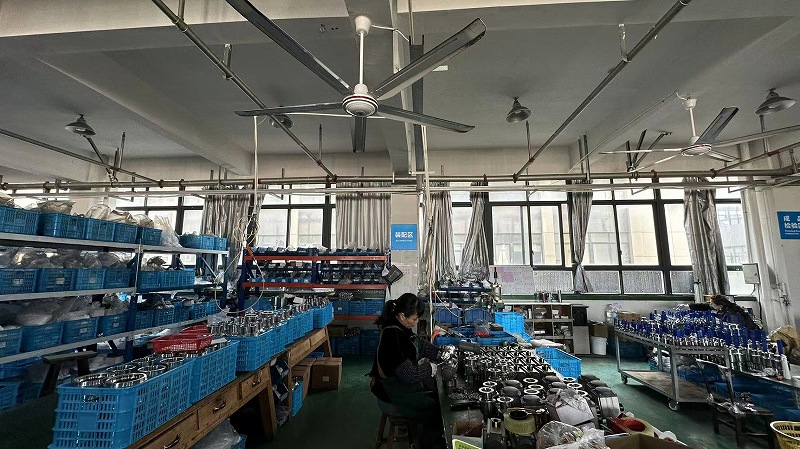
Our team consists of experienced engineers, skilled technicians, and dedicated professionals collaborating to deliver top-tier products. Our specialists focus meticulously on critical component designs, ensuring flawless technical specification adherence.
We adhere to stringent quality management systems. All products comply with international standards including ISO and API certifications, undergoing rigorous testing for performance, durability, and safety across chemical, oil, and water treatment sectors.
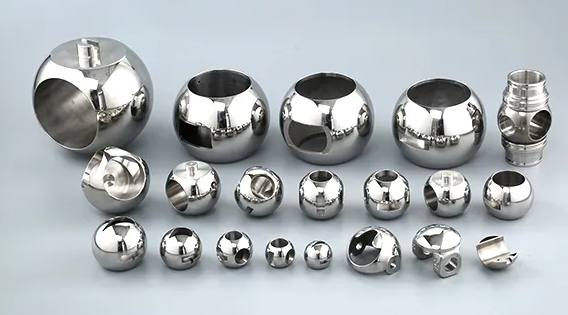
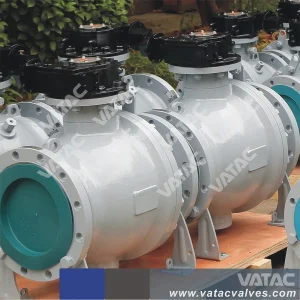
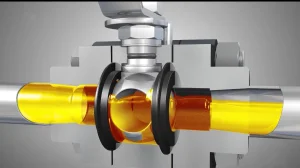
High-pressure trunnion and floating ball valves engineered to withstand extreme temperatures, corrosive sour gas, and high-velocity fluid slurries.
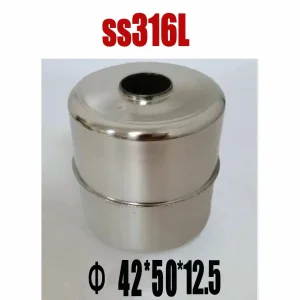
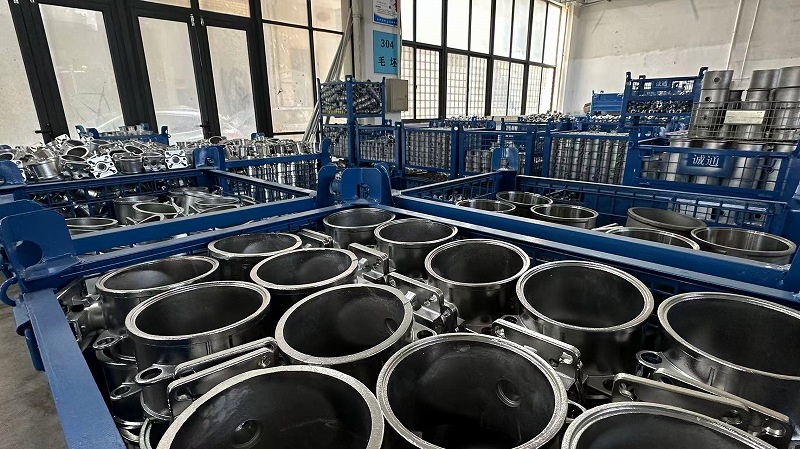
Reliable check valves, float balls, and corrosion-resistant assemblies designed for municipal dewatering, desalination, and heavy industrial effluent management.
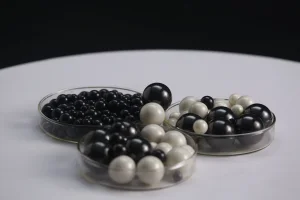
Inert ceramic (Alumina, Zirconia) and PTFE/POM valve components ensuring absolute chemical resistance against aggressive acids and alkaline solutions.
Continuous R&D into nanostructured coatings and ultra-pure ceramic composites to push the limits of wear resistance and friction reduction in extreme valve applications.
Implementing automated optical inspection (AOI), AI-driven CNC machining calibration, and IoT-enabled quality tracking across all production lines.
Optimizing energy efficiency in manufacturing processes and developing recyclable, long-life components that align with global net-zero industrial mandates.
At Hubei RPZ Valve Co., Ltd., we believe in forging strong, long-term relationships with our clients. Whether you are looking for standard products or customized solutions, we are ready to work closely with you to meet your specific needs. Our dedicated customer support team is available to assist with technical inquiries, order placement, and any other needs that may arise.
If you are interested in any of our products or would like to discuss a custom order, please do not hesitate to contact us. We welcome the opportunity to form successful business relationships with new clients and partners around the world. We look forward to helping you achieve success through our high-quality products and exceptional customer service.
Get in Touch Today